Grup Giró
Packaging
Machine vision and color-based classification systems for the automation of banana grading
The development of color-based grading systems using machine vision enables the automation of banana selection according to their stage of ripeness.
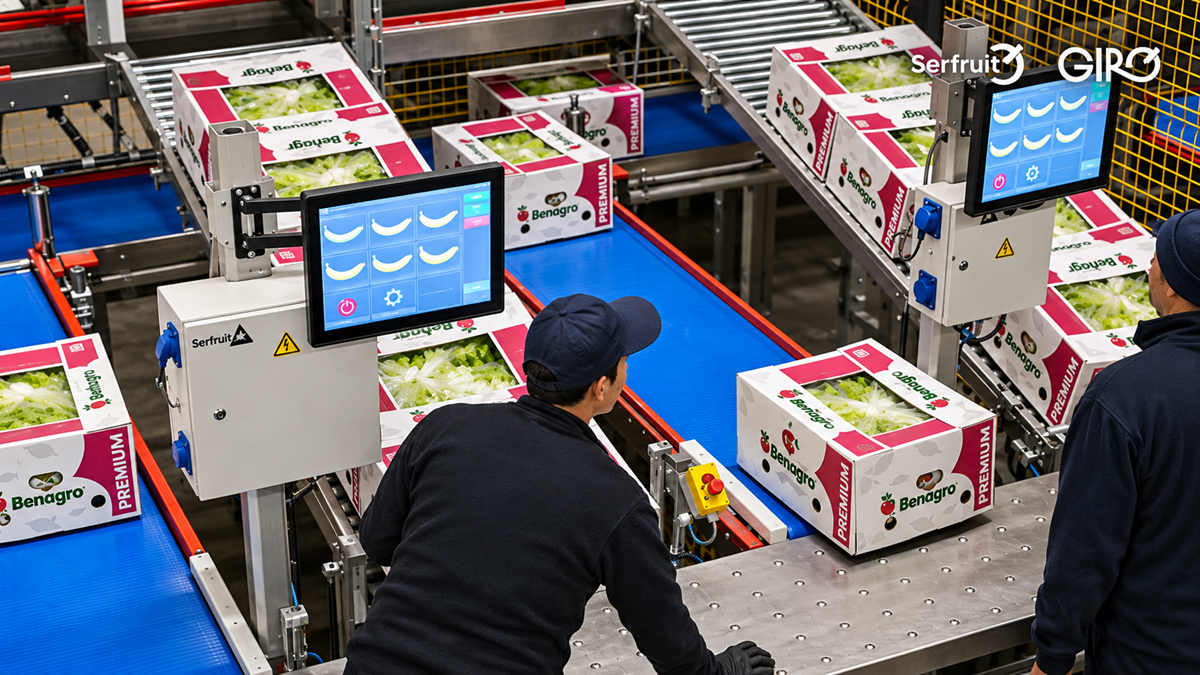
The industrialization of fresh fruit handling has taken a decisive step forward with the implementation of machine vision technologies designed for sorting based on ripeness. For a product as perishable and sensitive to handling as the banana, precise selection prior to packaging is critical to ensuring uniformity in batches destined for large-scale retail and minimizing losses throughout the supply chain.
In this context, a strategic partnership between Grupo Giró and Serfruit has led to the development of a color-based grading system specifically designed for banana processing lines. Using high-resolution optical sensors, this technology analyzes the exact color transition of each individual banana or bunch, classifying the fruit in real time according to its commercial ripeness all without physical contact that could damage the product's skin.
Integrating machine vision into automated color-based sorting addresses one of the primary bottlenecks in banana packing facilities, where manual sorting often leads to inconsistency and high labor requirements. By automating color detection, the system not only boosts the line’s hourly throughput but also ensures rigorous standardization of the final boxes or packages, allowing distributors to accurately predict the product's shelf life in retail stores.
By incorporating Serfruit’s image-processing software into Grupo Giró’s automated equipment, the industry demonstrates how the convergence of robotics, machine vision, and packaging machinery serves as a key technological solution for meeting the quality standards of the international tropical fruit market.
Another step toward the consolidation of projects
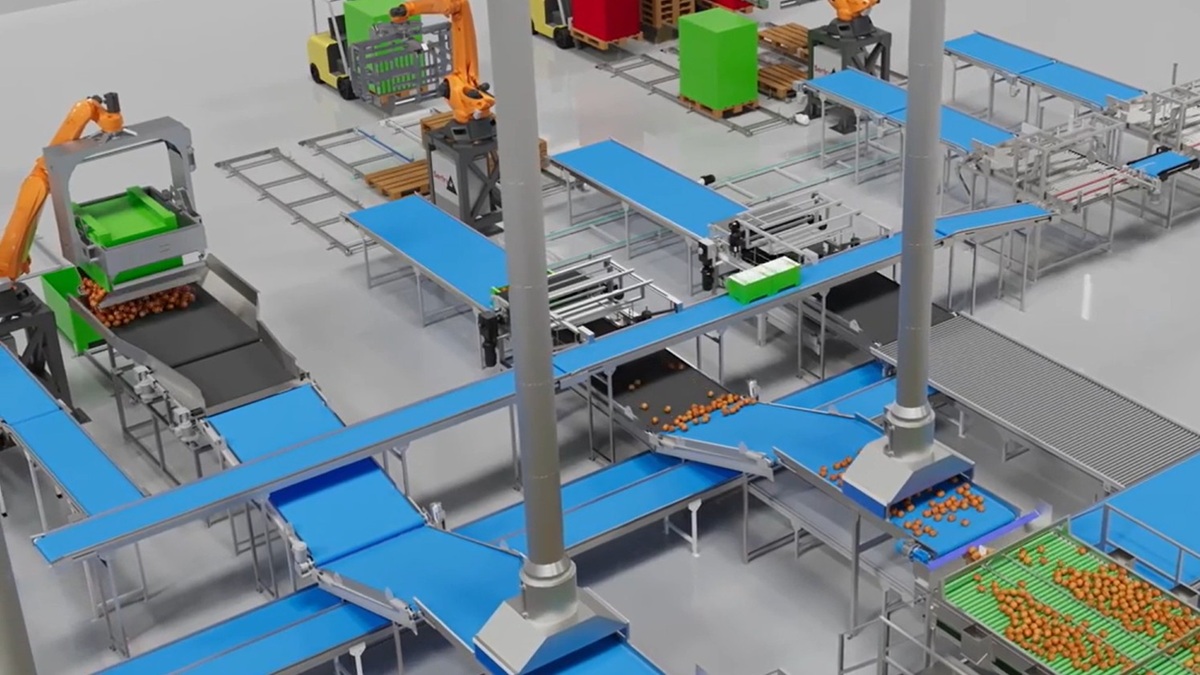
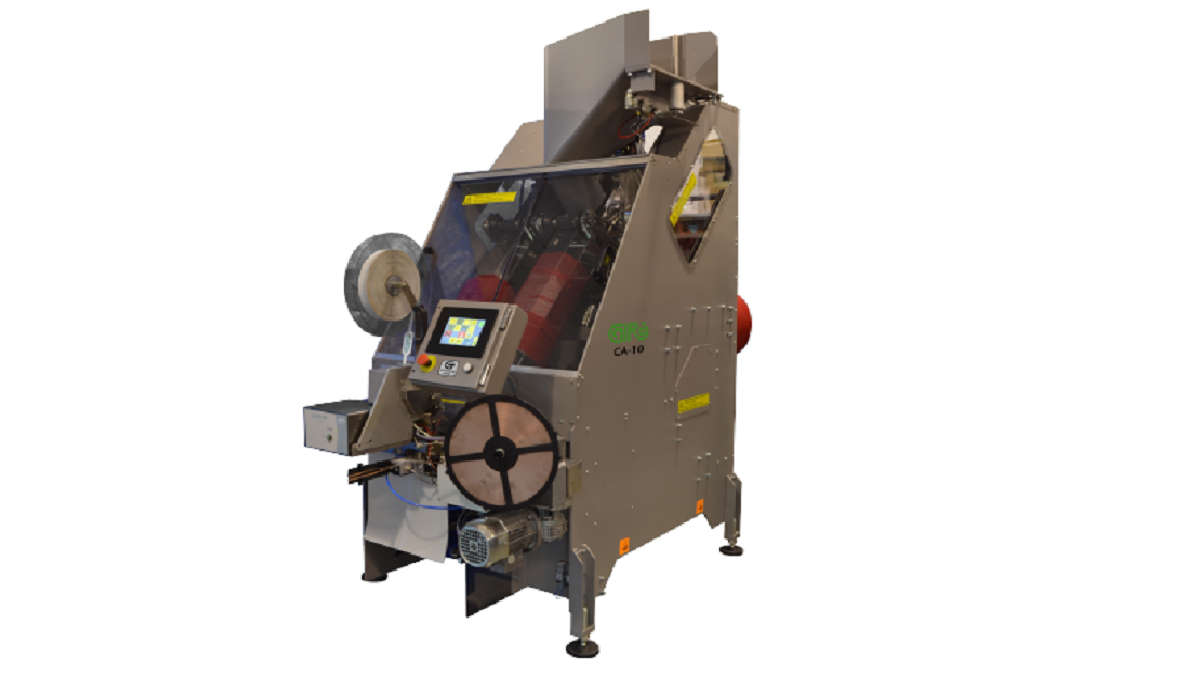
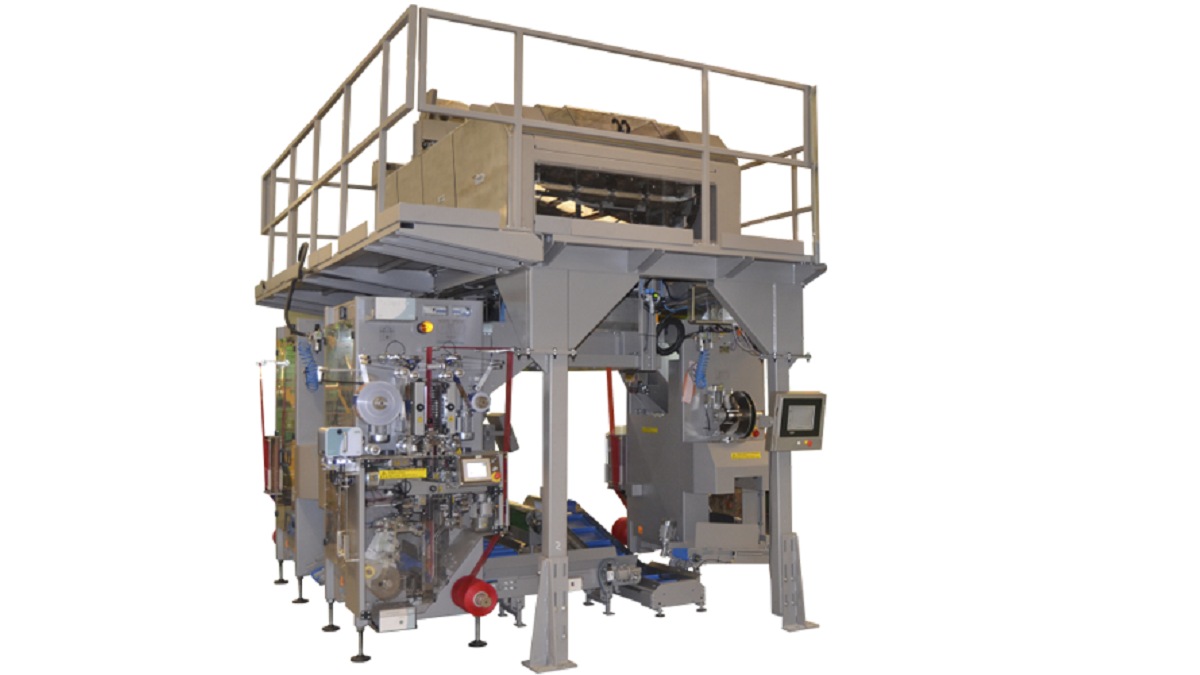
These types of joint developments highlight the consolidation of Grupo Giró as a comprehensive leader in post-harvest engineering and fresh produce packaging. By integrating Serfruit’s image-processing software and advanced mechatronics into its weighing and packaging platforms, the Spanish firm strengthens its ability to deliver "turnkey" projects tailored to the operational requirements of high-volume packing facilities worldwide.
Furthermore, the technological synergy between the two companies reflects the sector’s irreversible shift toward digitalization and real-time data control within packing plants. By combining dynamic weighing, optical vision-based sorting, and automated boxing, the supporting industry addresses the challenge of ensuring full product traceability while drastically reducing losses caused by handling, as well as the overall energy costs of the process.
News of Grup Giró